Views: 0 Author: Site Editor Publish Time: 2026-08-08 Origin: Site
Heavy-duty applications constantly demand immense power. Modern engineers face a relentless core challenge here. They must maximize torque output while navigating extremely strict spatial constraints in equipment design. Traditional parallel shaft or worm gearboxes frequently fall short in these demanding environments. Instead, planetary kinematics serve as the undisputed industry standard for high-torque requirements. Multiple gear meshes share the applied load simultaneously. This brilliant architecture dramatically multiplies rotational force without drastically expanding the gearbox footprint. You need a highly reliable framework to navigate these complex specifications. This article provides exactly that. We offer engineers and procurement teams an objective, step-by-step guide. You will learn how to specify, size, and properly integrate a heavy-duty system. We explore prime mover compatibility, thermal rating assessments, and standard modular architectures to ensure long-term industrial reliability.
Planetary gear reducers deliver the highest torque density per cubic inch, making them mandatory for space-constrained, high-load operations.
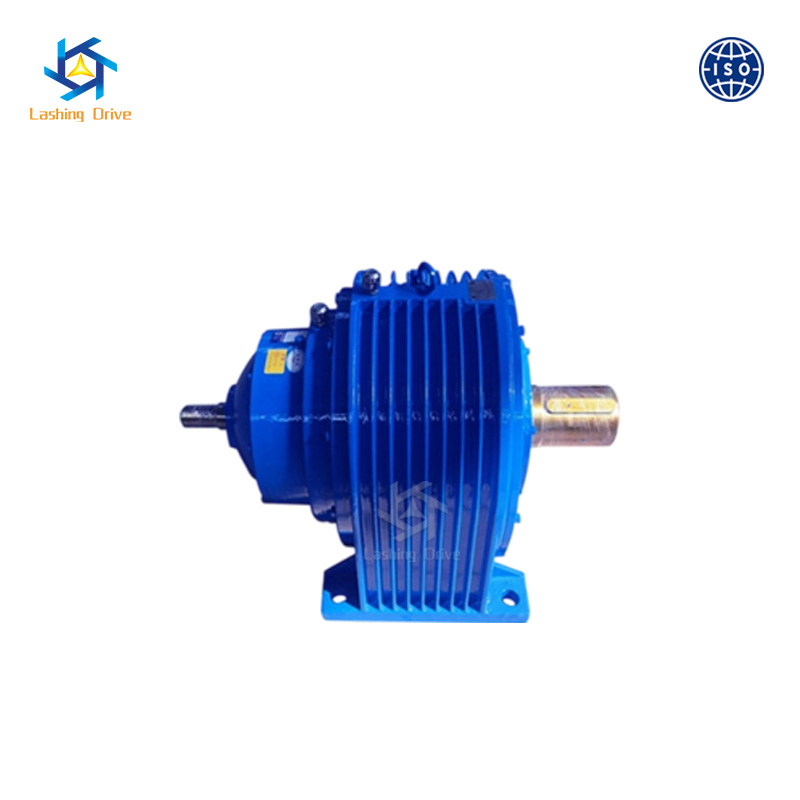
Selecting a P Series planetary gear reducer offers a modular, standardized approach that simplifies sizing for multi-stage, ultra-high torque requirements.
Prime mover compatibility dictates design: integration parameters differ vastly between electric servo motors and a hydraulic motor driven planetary reducer.
Proper evaluation requires assessing both mechanical rating (peak shock loads) and thermal rating (continuous operation limits) to prevent premature failure.
Understanding the fundamental mechanics of load distribution helps explain why certain architectures dominate heavy industries. A Planetary Gear Reducer relies on a central sun gear to initiate movement. This sun gear drives multiple surrounding planet gears simultaneously. These planet gears rotate safely inside a stationary outer ring gear. This specific layout inherently divides incoming torsional forces. The applied load spreads evenly across multiple contact points at all times. Because multiple teeth mesh together, the stress per individual gear tooth drops significantly. This mechanism allows for an exceptionally high shock load tolerance during heavy operations.
You can clearly see this advantage when comparing footprint sizes. Traditional helical gearboxes rely on single-point gear meshing. They require massive physical housings to accommodate wider, thicker gears for equivalent power. In contrast, a High Torque Planetary Reducer delivers an immensely dense torque-to-weight ratio. They typically occupy up to fifty percent less spatial volume than parallel shaft equivalents. You save vital installation space on crowded machinery decks and mobile equipment frameworks.
Typical high-torque use cases reflect these physical advantages clearly. Heavy industrial sectors rely almost entirely on these compact powerhouses. We frequently see them driving massive mining conveyors across rugged terrains. Mobile crane winches depend entirely on their concentrated lifting power to handle suspended loads safely. Heavy extrusion machinery uses them continuously to push dense raw materials through tight dies. In every scenario, the combination of extreme power and compact size makes planetary kinematics the only viable engineering choice.
Industrial applications benefit massively from standardized engineering frameworks. When you evaluate a P Series Planetary Gear Reducer, you look primarily at its modular architecture. This specific series designation represents a highly adaptable industrial standard. Engineers can easily configure them for either coaxial or right-angle inputs depending on motor placement. The modular design allows you to stack multi-stage planetary assemblies together seamlessly. You can scale the final torque output exponentially without fundamentally redesigning the entire driveline.
Standardization brings massive practical advantages over full custom design. Utilizing a standard P Series framework drastically reduces engineering lead times. Manufacturers maintain pre-engineered 3D CAD models and predictable torque brackets for these units. This accessibility simplifies the initial design phase immensely. Furthermore, it streamlines replacement part procurement years down the line. You eliminate the agonizing wait times often associated with one-off custom gearings. Maintenance teams can easily source standard planetary carriers, sun gears, or bearing assemblies globally.
Choosing the correct output configuration remains a critical step in this evaluation. It depends entirely on your specific radial and axial load demands. You must match the interface to the driven machine accurately.
Solid shaft with keyway: Ideal for standard, unidirectional torque transfer where loads remain relatively uniform.
Splined shaft: Better suited for frequent reversing loads. They prevent the wallowing out often seen in keyways under severe shock environments.
Shrink disc hollow shaft: Provides a rigid, completely backlash-free friction connection. This method proves exceptional for carrying heavy radial loads without fatigue.
Prime mover compatibility dictates the entire external design of the reducer housing. You must approach integration differently based on the power source. Let us first examine Hydraulic Motor Driven Planetary Reducer systems.
These hydraulic systems offer distinct advantages in specific environments. They provide exceptionally high starting torque directly from a standstill. They operate incredibly robustly in harsh, highly explosive environments where electrical sparks pose catastrophic risks. Additionally, low-speed control mechanisms remain highly simplified through basic fluid valve adjustments. However, integration realities require careful planning. You must specify exact input flanges to match specific hydraulic motor splines. Managing hydraulic fluid temperature becomes essential during continuous long shifts. You also need specialized, heavy-duty leak-prevention sealing to handle high fluid pressures.
Conversely, electric motor and servo drive systems dominate automated manufacturing. They offer incredibly precise positional control for complex machinery. Maintenance overhead typically remains lower without the presence of hydraulic fluid. You can integrate them effortlessly into automated PLC networks. Yet, their integration realities present unique mechanical challenges. Careful inertia matching proves mandatory. The planetary gear ratio directly squares the load inertia reflected back to the motor. You must evaluate backlash tolerances closely. Poor integration causes motor hunting, excessive vibration, or sudden drive faults.
Feature | Hydraulic Drive System | Electric/Servo Drive System |
|---|---|---|
Starting Torque | Exceptionally high instantly | High, but limited by peak current limits |
Environment Suitability | Excellent for explosive/harsh areas | Best for clean, automated environments |
Control Precision | Basic low-speed control | Highly precise positional accuracy |
Integration Challenge | Fluid temperature and specialized sealing | Inertia matching and backlash evaluation |
Engineers frequently fall into a common technical trap when sizing these units. They focus entirely on mechanical capacity while ignoring the thermal limit. A gearbox might mechanically handle a massive peak torque rating quite safely. The gears and shafts possess the sheer physical strength to endure the twisting force. However, that same gearbox will rapidly overheat during continuous duty cycles. Compact housings inherently struggle to dissipate heat naturally. Internal oil temperatures rise, breaking down lubrication films. You must evaluate both ratings rigorously. Always ensure your continuous operating torque remains comfortably below the manufacturer's thermal dissipation limit.
Applying realistic service factors prevents these premature failures entirely. You cannot rely purely on nominal torque numbers. Recognized standards from AGMA or ISO dictate how we apply these crucial safety multipliers. Operational hours directly influence these multipliers. Shock load frequency also dramatically changes the required service factor.
Evaluate the duty cycle: Determine exactly how many hours the machine runs daily. Continuous 24/7 operation demands a higher multiplier than intermittent use.
Assess the load type: Classify the operation accurately as uniform, moderate shock, or heavy shock. A rock crusher experiences vastly different loads than a water pump.
Apply the multiplier: Increase your base nominal torque requirement according to the combined operational severity. Size your reducer based on this final calculated number.
You must also define acceptable backlash and torsional stiffness levels. Low backlash represents the physical play between meshing gear teeth. Precision positioning applications require strictly low backlash configurations. Torsional stiffness prevents the internal components from twisting like a spring under load. Conversely, standard backlash proves completely acceptable for continuous heavy conveying. You do not need absolute rigidity when merely moving bulk raw materials forward.
Theoretical lifespan means nothing without proper real-world implementation. Lubrication strategies represent the first major hurdle. Splash lubrication works exceptionally well for standard horizontal mounting positions. The internal gears drag oil upward, coating the upper components naturally. However, vertical orientations change this dynamic completely. Gravity pulls oil away from the upper bearings. Consequently, vertical mounts often require forced lubrication systems with internal pumps. Operating RPM also dictates the optimal fluid delivery method. High rotational speeds create windage, physically pushing oil away from critical mesh points. You must match the lubrication strategy to both orientation and speed.
Installation tolerances represent another massive operational risk factor. Misalignment creates devastating consequences for planetary assemblies. You must align the prime mover shaft perfectly with the reducer input. Angular or parallel misalignment accelerates bearing wear aggressively. It creates unbalanced internal loads, negating the theoretical lifespan completely. We highly recommend using precision laser alignment tools during the initial commissioning phase.
Condition monitoring serves as your best defense against unexpected downtime. We strongly recommend adding predictive maintenance technologies to mission-critical assets. Modern sensors prevent catastrophic failures before they happen.
Vibration sensors: Install these directly on the housing to detect early-stage bearing fatigue or gear pitting.
Oil debris analysis: Use magnetic plugs or inline sensors to track internal metal wear accurately over time.
Thermal probes: Monitor housing and oil temperatures in real-time to prevent unexpected thermal limit breaches.
Specifying the right heavy-duty reducer requires a delicate, informed balance. You must weigh immense torque density against strict prime mover compatibility requirements. Thermal management remains equally critical to physical gear strength. Overlooking any of these core variables guarantees premature equipment failure.
We advise buyers to apply strict shortlisting logic when evaluating manufacturers. Prioritize partners who provide fully transparent kinematic data upfront. Request comprehensive 3D CAD models immediately to validate your spatial integration parameters. Demand robust application engineering support rather than just a basic catalog selection.
Your next step should focus on validation. Encourage your design teams to consult directly with an application engineer. Run comprehensive dynamic load simulations based on your specific duty cycle. Finalize your procurement only after these simulations prove both mechanical and thermal viability.
A: Standard industrial units scale significantly to meet extreme demands. Multi-stage configurations can easily extend up to millions of Newton-meters (Nm). They achieve this massive capacity by stacking multiple planetary stages together, multiplying the force sequentially while distributing the load safely.
A: The core planetary stages remain identical in both configurations. The differences lie strictly in the input stage. Hydraulic units require specific adapter flanges, splined input captures, and heavy-duty leak sealing mechanisms to handle high-pressure fluid environments safely.
A: Compact gearbox housings possess limited surface area. They struggle to dissipate internal heat naturally during continuous, heavy-duty cycles. While the physical steel gears possess the mechanical strength to handle the load, the enclosed oil will rapidly overheat and degrade without proper cooling.
A: Yes, they absolutely can handle extreme forces. However, this capability depends entirely on the chosen output bearing configuration. P Series units utilizing heavy-duty taper roller bearings manage massive external radial loads highly efficiently without internal deflection.